01
Consultation
Technical needs assessment

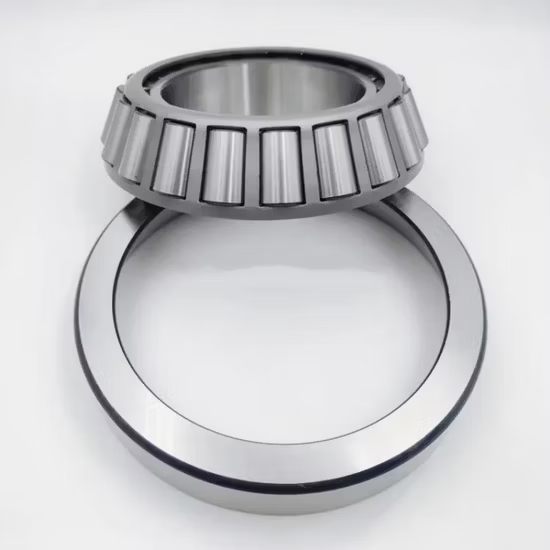
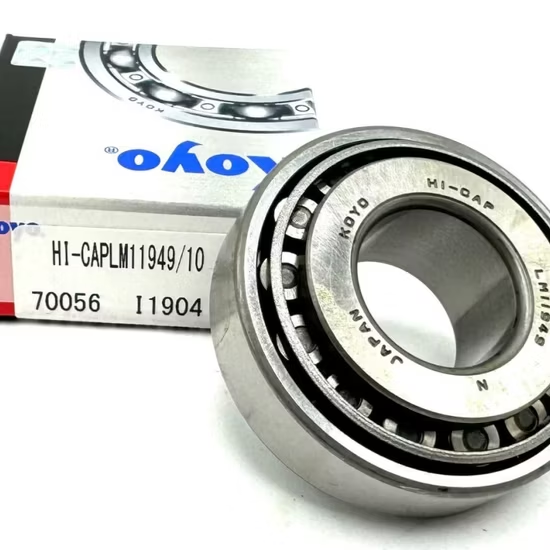
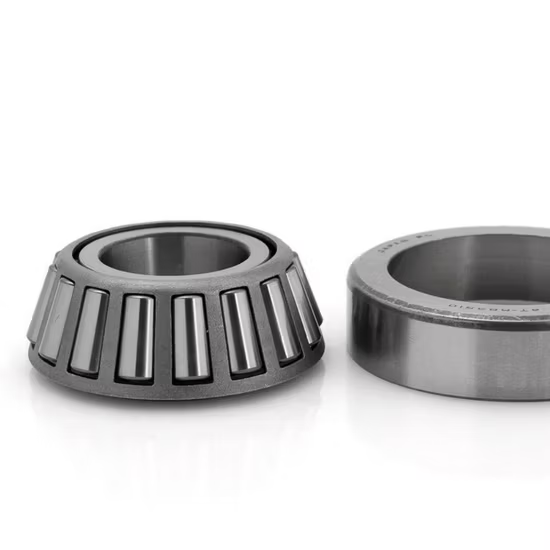
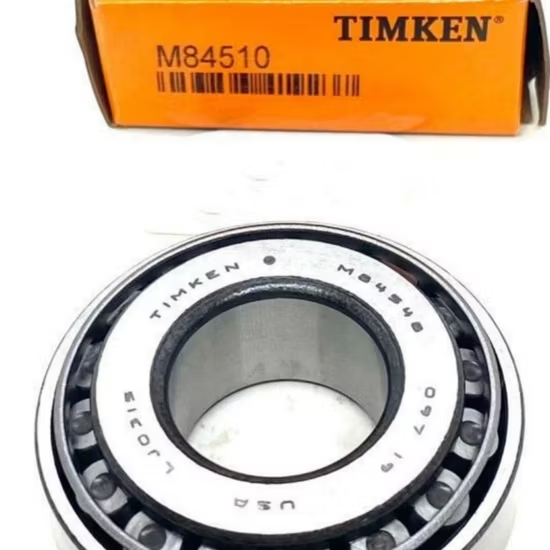
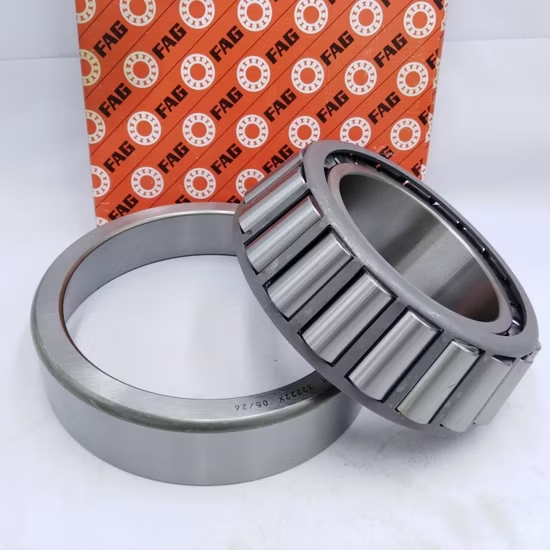
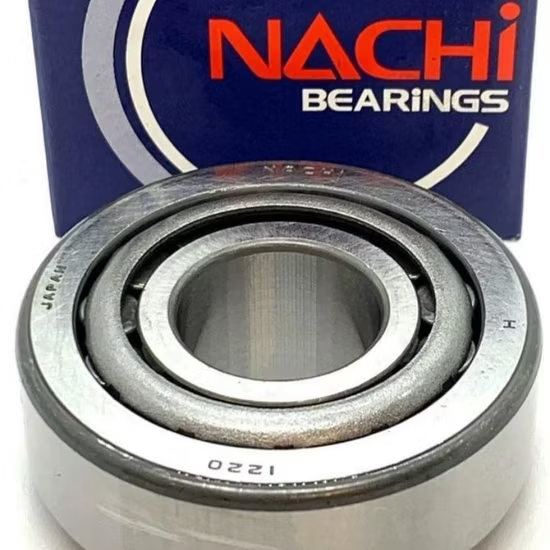
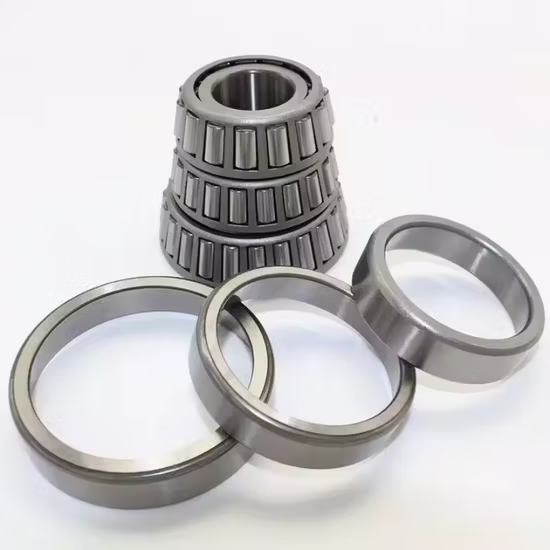
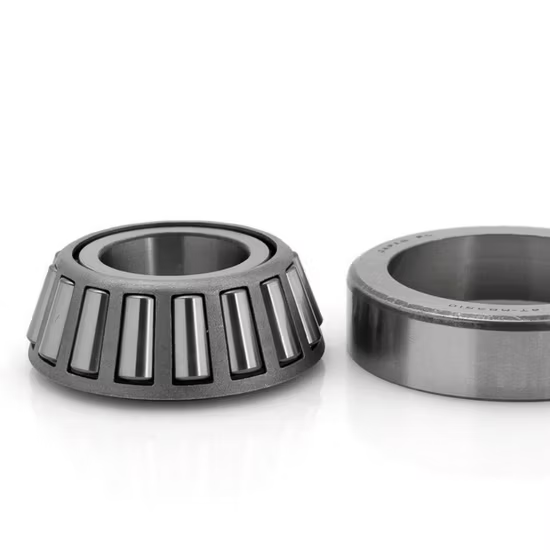
15101/15243 Single Row Inch Tapered Roller Bearing — cone and cup pair engineered for combined radial and axial loads in heavy-duty applications.
Full material test reports and dimensional inspection certificates accompany every shipment.
Cross-Reference Alignment Verified — matching internal clearance and cage design alongside the base cone and cup numbers prevents field binding.
| Parameter | Value |
|---|---|
| Designation | 15101/15243 |
| Bearing Type | Inch Tapered Roller Bearing |
| Number of Rows | Single Row |
| Precision Class | P4 |
| Material | GCr15 bearing steel |
| Cage Material | Available in pressed steel or brass options |
| Bore Type | Cylindrical (inch dimensions) |
| Arrangement | Separable cone and cup components |
| Industry | Typical Applications |
|---|---|
| Mining and Crushing | Primary jaw crusher pitman shafts and heavy vibrating screen exciter mechanisms |
| Heavy Vehicle Repair | Drive axles, wheel hubs, and differential pinion shafts in off-highway trucks |
| Industrial Gearboxes | High-torque reduction gear sets and heavy-duty conveyor drive pulleys |
| Material Handling | Overhead crane travel wheels and heavy-load slewing support structures |
Thermal binding occurs when cross-referencing ignores internal geometry and precision tolerances.
In Latin American mining sites, I have witnessed numerous catastrophic shutdowns caused by assuming a basic part number was sufficient for heavy-duty applications. Procurement teams often source replacements that match the outer dimensions perfectly, yet the internal roller profile and precision grade fall short of the original equipment requirements. When a standard precision component is forced into a high-speed, heavy-load spindle or gearbox, the microscopic deviations in running accuracy generate excessive friction heat. This thermal accumulation rapidly degrades the lubricant, leading to premature cage failure and eventual shaft seizure long before the expected service interval.
Single row inch tapered structures are specifically engineered to manage simultaneous radial and thrust loads, making them indispensable in heavy machinery. Sourcing the correct 15101/15243 inch tapered roller bearing requires verifying that the internal load-carrying capacity aligns with the specific shock loads present in mining or crushing environments. We ensure that every cross-brand interchange we supply maintains the exact internal contact geometry required to distribute these complex forces evenly across the raceways.
Equipment operating in material handling and off-highway transport faces severe combined loading, where sudden directional shifts impose intense axial thrust alongside continuous radial weight. These applications generate substantial operational heat, which can diminish internal clearance if the initial mounting tolerances are not calculated for thermal expansion. Furthermore, the presence of abrasive dust in mining environments demands rigorous sealing solutions at the housing level, as open tapered designs rely entirely on external labyrinth seals to prevent contaminant ingress. Proper lubrication intervals and the correct grease viscosity are equally critical to maintain the hydrodynamic film under high-pressure contact zones.
The 15101/15243 inch tapered roller bearing designation represents a specific cone and cup pairing optimized for inch-dimension shafts and housings. The availability of P4 precision class ensures noticeably tighter dimensional and running accuracy compared to standard commercial grades, which is vital for minimizing vibration in high-speed gearboxes. Constructed from GCr15 high-carbon chromium bearing steel, the components offer enhanced wear resistance and fatigue life under continuous heavy loading. Depending on the specific speed and vibration profile of the application, the cage is available in pressed steel or brass options, allowing engineers to select the optimal retention design for their operating conditions.
Substituting a lower-precision or incorrect-clearance component might seem like a minor procurement saving, but it inevitably leads to unplanned downtime and catastrophic damage to adjacent shafts and housings. When the internal geometry fails to accommodate the thermal expansion of the shaft, the resulting preload spikes cause rapid surface spalling and roller skewing. This cascading failure not only voids equipment warranties but also forces emergency maintenance interventions in remote or hazardous locations.
Our cross-brand interchange process strictly aligns internal design, cage material, and precision suffixes, rather than just matching the base cone and cup numbers. We address the critical pain point of counterfeit components with soft inner rings by providing authorized coverage with full batch traceability. For applications requiring strict thermal management, we review the mounting tolerances to ensure the selected clearance class prevents field binding. Every shipment is backed by application-based selection reviews that account for the specific load, speed, and temperature conditions of your machinery.
To ensure the selected component perfectly matches your operational demands, please provide the specific radial and axial load profiles, operating speeds, and ambient temperature ranges. Sharing the original equipment manufacturer part numbers allows our engineering team to perform a comprehensive cross-reference check, verifying that all internal geometries and precision classes align. This technical review guarantees that the replacement integrates flawlessly into your existing assembly without requiring housing modifications.
Q: How can we verify the authenticity of the received components?
A: Every shipment includes batch traceability documentation and a unique QR code that can be scanned using the manufacturer's official mobile application. This digital verification confirms the origin and production lot, protecting your operation from counterfeit parts with soft inner rings that pass casual visual inspection but fail under heavy load.
Q: Why is cross-referencing more complex than just matching the base numbers?
A: Matching only the base cone and cup numbers often overlooks critical internal differences such as cage material, roller profile, and precision grades. A component with the correct outer dimensions but standard precision will generate excessive heat and fail prematurely when installed in a high-speed application requiring P4 accuracy.
Q: What is the practical difference between P4 and standard precision classes?
A: P4 precision guarantees noticeably tighter dimensional and running accuracy, which significantly reduces vibration and heat generation during high-speed rotation. This enhanced accuracy is essential for maintaining the hydrodynamic lubrication film in industrial gearboxes, thereby extending the fatigue life of the rolling elements.
Q: How do we choose between pressed steel and brass cage options?
A: Pressed steel cages are generally suitable for standard speeds and offer a lightweight design, while brass cages provide superior durability and vibration resistance in high-load, low-speed, or high-temperature environments. The choice depends on the specific shock loads and thermal conditions present in your machinery.
Q: What mounting practices prevent thermal binding in tapered designs?
A: Preventing thermal binding requires calculating the exact shaft and housing tolerances to maintain the correct internal clearance after mounting and during thermal expansion. Using induction heating exclusively on the inner ring and verifying the axial seating against the shaft shoulder ensures the geometry remains stable under operational temperatures.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.