01
Consultation
Technical needs assessment

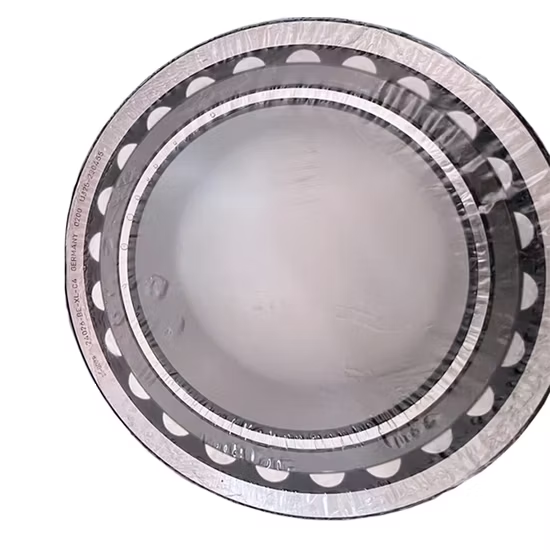
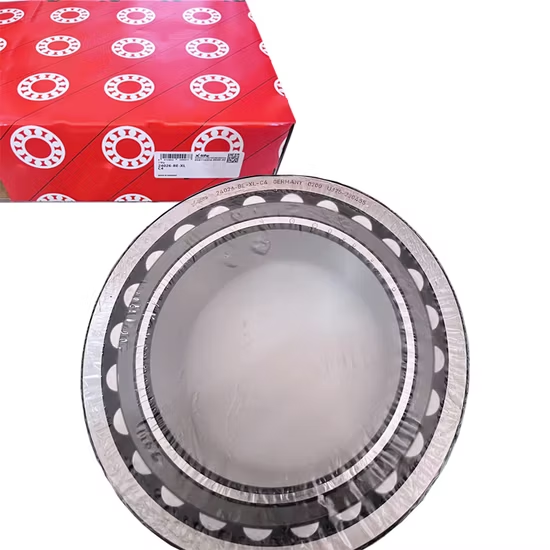
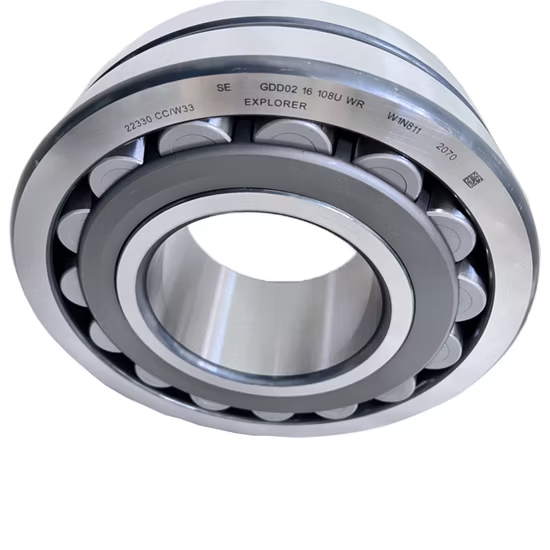
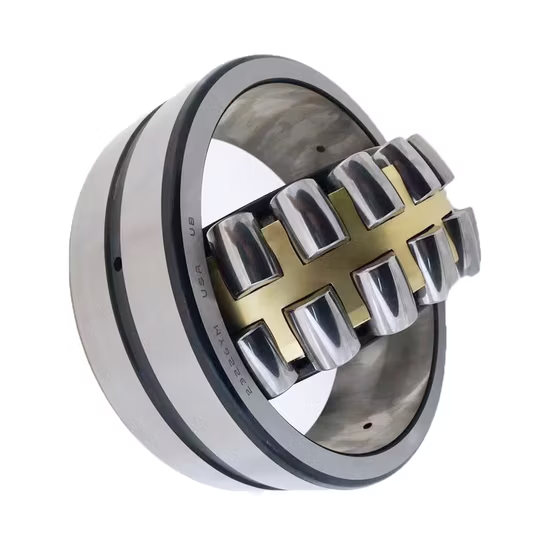
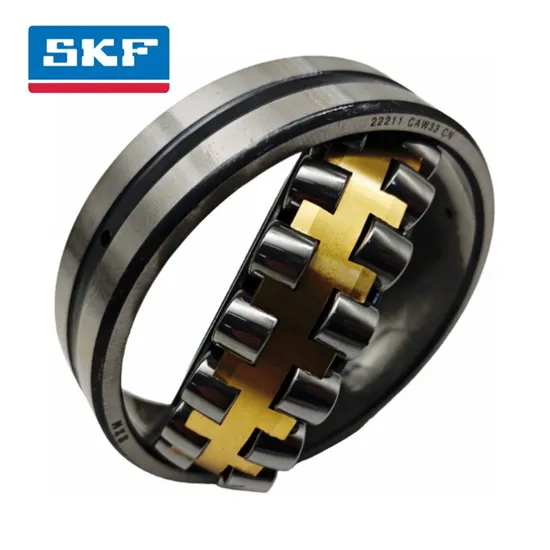
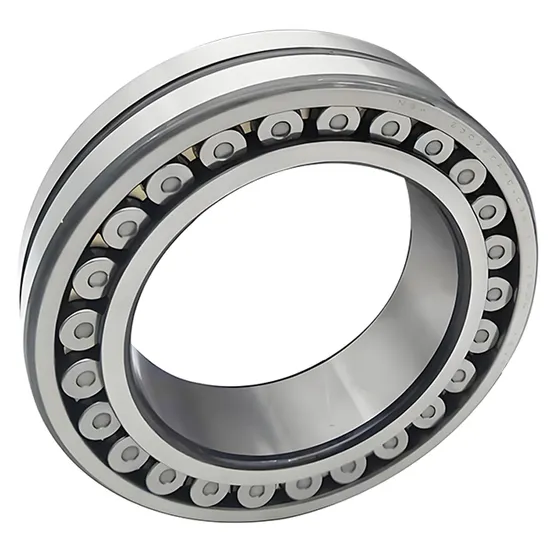
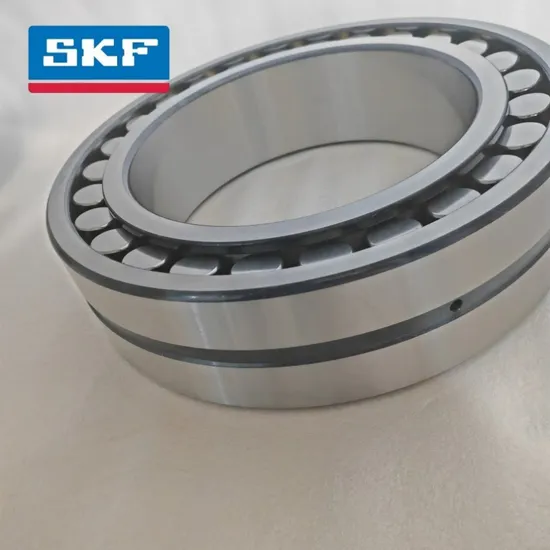
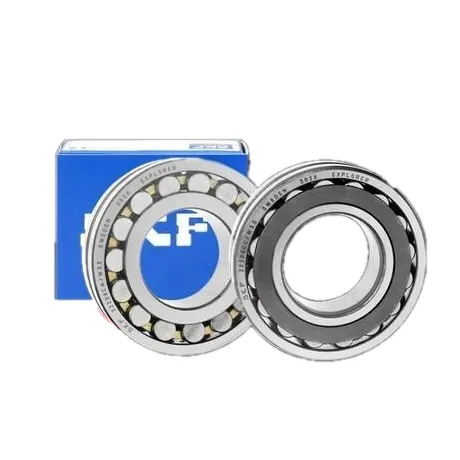
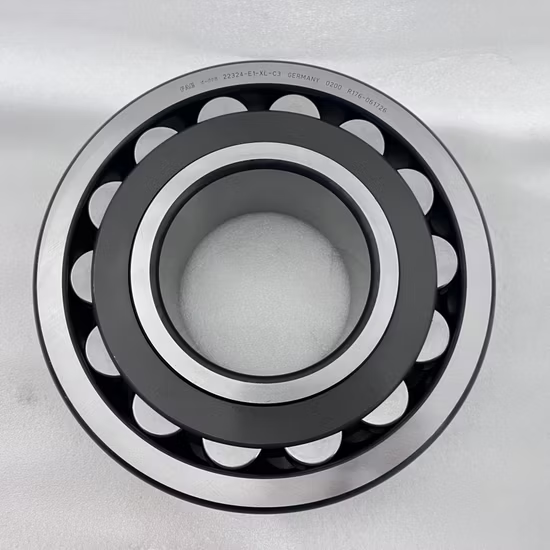
S K F 22220 22222 22224 22228 22230 E Cc Ca MB 3528 3530 W33 Spherical Roller Bearing — The E optimized internal design maximizes dynamic load capacity, while the W33 outer ring lubrication groove ensures efficient grease distribution. Buyers can select between Cc stamped steel and MB machined brass cages to match specific vibration and heavy load conditions.
Traceable Batch Documentation — Every S K F 22220 22222 22224 22228 22230 E Cc Ca MB 3528 3530 W33 spherical roller bearing ships with verifiable manufacturer lot records, eliminating the guesswork in heavy-duty spares procurement.
| Parameter | Value |
|---|---|
| Designation | S K F 22220 22222 22224 22228 22230 E Cc Ca MB 3528 3530 W33 |
| Bearing Type | Spherical Roller Bearing |
| Cage Material | Stamped steel (Cc) or Machined brass (MB) |
| Internal Design | Optimized (E) |
| Lubrication Features | Outer ring groove and holes (W33) |
| Origin | Germany/Japan/Sweden/Malaysia/China |
| HS Code | 8482500090 |
| Service | OEM |
| Industry | Typical Applications |
|---|---|
| Mining and Crushing | Jaw crusher toggle plates, vibrating screen exciter mechanisms |
| Steel and Metallurgy | Continuous caster roll segments, rolling mill gearbox shafts |
| Industrial Gearboxes | Heavy-duty reduction gear intermediate shafts, extruder drives |
| Paper Machines | Dryer cylinder journal supports, press roll bearings |
Matching the base bore and outside diameter while ignoring the cage or lubrication suffix is the fastest route to a seized shaft. A S K F 22220 22222 22224 22228 22230 E Cc Ca MB 3528 3530 W33 spherical roller bearing will fail prematurely if the internal design does not align with the actual thermal and vibrational loads of the equipment.
I have stood in African mining sites watching a massive screen deck lock up solid because a standard CN clearance and stamped steel cage were forced into an application demanding C3 expansion tolerance and brass guidance. The heat generated under heavy radial loads simply welded the rollers to the cage. When procurement teams treat suffixes as optional suggestions rather than critical engineering parameters, the resulting unplanned downtime costs exponentially more than the correct component.
Selecting the right S K F 22220 22222 22224 22228 22230 E Cc Ca MB 3528 3530 W33 spherical roller bearing requires looking past the catalog number to the actual operating environment. Our technical review process verifies that the chosen internal geometry and cage material can withstand the specific shock loads and misalignment angles present in your machinery, preventing early fatigue spalling.
Heavy industrial environments subject these components to severe combined loading, where high radial forces intersect with moderate axial thrust and constant vibration. Elevated operating temperatures drastically alter the internal clearance, making the correct thermal expansion allowance critical to prevent binding. Furthermore, contaminated environments demand reliable re-lubrication pathways to flush out abrasive particulates before they score the raceways.
The E designation signifies an optimized internal geometry that maximizes the dynamic load rating by improving roller guidance and stress distribution. The Cc suffix identifies a stamped steel cage, which is roller-guided and highly effective for standard industrial speeds and moderate vibrations. Conversely, the MB suffix denotes a machined brass cage guided by the inner ring, offering superior tensile strength and resistance to cage fracture under severe shock loads or high-vibration screening applications. The W33 feature provides a lubrication groove and three holes in the outer ring, ensuring that fresh grease reaches the roller ends efficiently during maintenance intervals.
Installing a component with the wrong internal clearance or inadequate cage strength leads directly to catastrophic thermal seizure or cage disintegration. According to ISO 15243 frameworks, these failures are classified as preventable mounting or selection errors, which immediately voids equipment warranties. The resulting collateral damage to shafts and housings turns a simple swap into a major rebuild project.
We eliminate the risk of receiving cloned components with soft inner rings by providing full manufacturer batch traceability for every unit. Cross-referencing is executed by verifying the exact cage material and clearance class, not just the base dimensions, ensuring your vibrating screens do not inherit a mismatched stamped cage. Our application-based selection review catches thermal binding risks before the order is placed, and we consolidate mixed-brand requirements into a single, fully documented shipment to simplify your MRO inventory.
To ensure precise specification matching, provide your radial and axial load profiles, operating speeds, and expected thermal gradients for a comprehensive L10 life calculation. Supplying the original OEM equipment designation allows our engineering team to execute a strict cross-reference check, confirming that the internal design, cage guidance, and lubrication features perfectly align with your machinery's original requirements.
Q: Why must both the cage and lubrication suffixes be verified during cross-referencing?
A: Matching only the base bore and OD while ignoring suffixes like MB or W33 leads to catastrophic field failures. A machined brass cage is essential for high-vibration screens to prevent fracture, while the W33 groove ensures adequate grease distribution. Overlooking these details results in thermal seizure or rapid cage wear under heavy industrial loads.
Q: How do I verify the authenticity of these specific spherical roller bearings?
A: Every unit is supplied with a Certificate of Conformity and batch traceability documentation. You can verify the physical component by scanning the manufacturer's QR code using their official mobile application, which confirms the production facility, date, and exact suffix configuration against the central database.
Q: What is the selection boundary between MB and Cc cages in vibrating equipment?
A: The Cc stamped steel cage is suitable for standard moderate-vibration applications, offering lower friction. However, for high-amplitude vibrating screens or crushers subjected to severe shock loads, the MB machined brass cage is mandatory. Its superior tensile strength and inner-ring guidance prevent the cage from fracturing under extreme dynamic stress.
Q: How does the W33 design impact relubrication intervals in heavy machinery?
A: The W33 outer ring groove and three lubrication holes distribute fresh grease directly to the roller ends, effectively flushing out abrasive contaminants. This targeted delivery improves lubrication efficiency in dirty environments like mining or cement, potentially extending maintenance intervals and preventing premature raceway scoring compared to bearings without this feature.
Q: How do I identify the correct clearance class for high-temperature applications?
A: Standard CN clearance will cause thermal binding when inner ring expansion occurs at elevated operating temperatures. You must specify C3 or C4 clearance suffixes to provide the necessary internal expansion room. Share your operating temperature and shaft fit data so we can calculate the exact residual clearance required to prevent the bearing from locking up during operation.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.