01
Consultation
Technical needs assessment
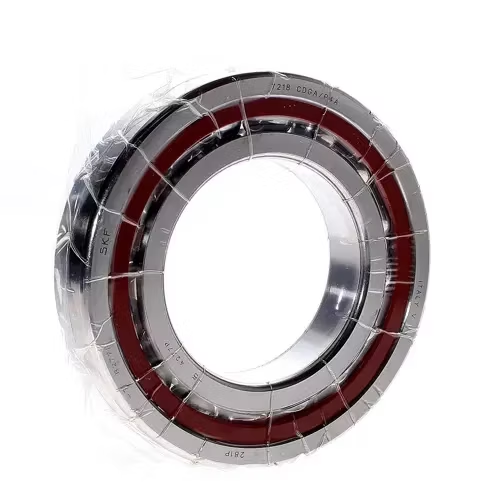
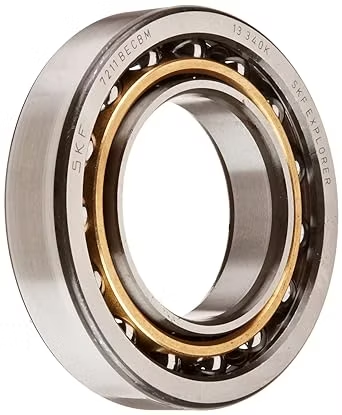
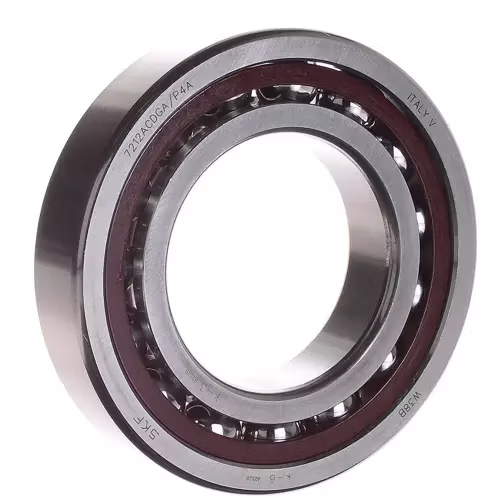
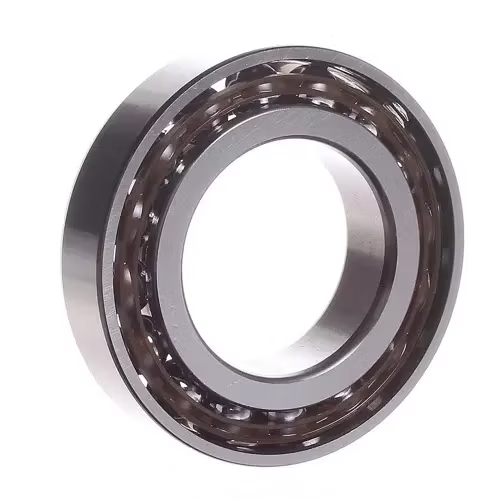
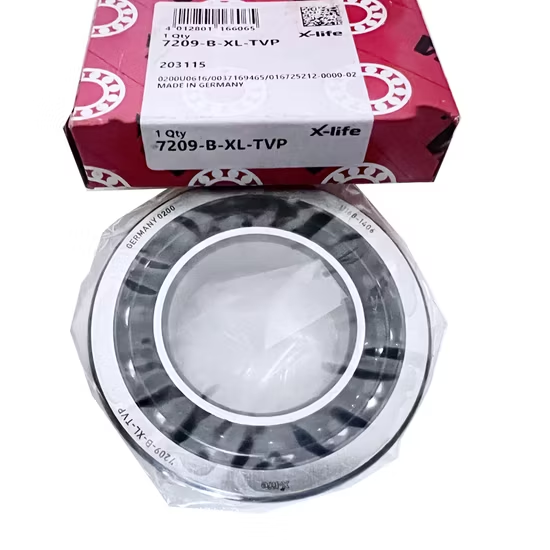
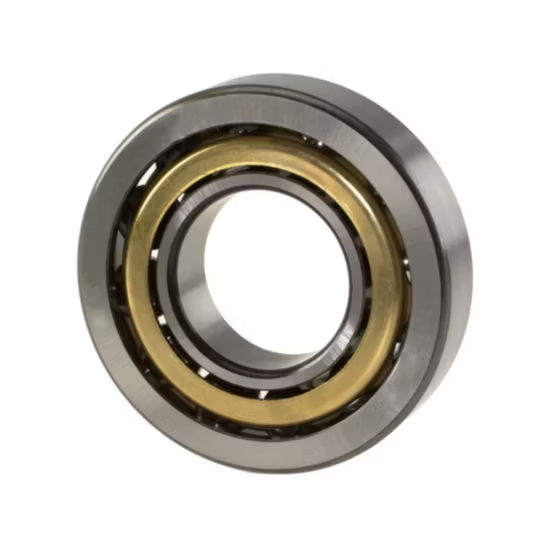
7212 Becbm Angular Contact Ball Bearing 60×110×22 mm — engineered with a 40° contact angle to handle combined radial and axial loads, while the optimized internal design maximizes load carrying capacity for high-speed equipment.
Universal Pairing Match — every 7212 Becbm angular contact ball bearing ships with verified preload grouping to prevent thermal binding in paired spindle setups.
| Parameter | Value |
|---|---|
| Designation | 7212 Becbm |
| Product Type | Angular Contact Ball Bearing |
| Bore Diameter (d) | 60 mm |
| Outside Diameter (D) | 110 mm |
| Width (B) | 22 mm |
| Contact Angle | 40° |
| Number of Rows | Single |
| Material | Bearing Steel |
| Cage Material | Machined Brass |
| Arrangement | Universal Pairing |
| Origin | Germany / Japan / Sweden / Malaysia / China |
Note: The lowercase 'cb' and 'm' suffixes in the 7212 Becbm identifier are non-standard notations; they correspond to the universal heavy preload (CB) and machined brass cage (M) classifications in standard manufacturer catalogs.
| Industry | Typical Applications |
|---|---|
| Machine Tool Manufacturing | High-speed CNC spindle assemblies, precision grinding headstocks |
| Industrial Pump Systems | Multi-stage centrifugal pump thrust collars, boiler feed pump shafts |
| Robotics & Automation | Articulated joint actuators, high-torque servo motor gearboxes |
| General Power Transmission | Heavy-duty industrial gearbox pinion shafts, compressor rotors |
Matching the base dimension without verifying the exact preload and cage suffix is the primary cause of catastrophic thermal seizure in high-speed spindles.
Procurement teams often approve alternative bearings based solely on the 7212 dimension series, ignoring the critical pairing arrangements. When a standard single bearing is forced into a back-to-back spindle configuration requiring matched universal pairing, the lack of factory-ground flush faces and controlled internal clearance leads to uneven load distribution. The resulting friction generates excessive heat, rapidly degrading the lubricant and causing the cage to collapse under centrifugal force . Sourcing the precise 7212 Becbm angular contact ball bearing eliminates this hidden risk by ensuring the internal geometry aligns perfectly with the equipment's thermal expansion tolerances.
Precision machining environments demand absolute rotational stability and high axial rigidity. The 7212 Becbm angular contact ball bearing is engineered to handle the combined radial and heavy axial loads typical in CNC milling and grinding operations. Our technical review process ensures that the specific preload class of this designation matches your spindle's operational speed, preventing the micro-slip and smearing damage that plagues incorrectly paired bearing sets.
High-speed rotation generates significant internal friction, requiring careful management of thermal expansion. The 40° contact angle provides the necessary axial stiffness, while the machined brass cage ensures structural integrity and reliable oil-mist or grease lubrication flow at elevated RPMs. If the internal clearance is too tight for the operating temperature, the bearing will preload itself to destruction; if too loose, vibration will compromise surface finish . Selecting the correct universal pairing class ensures the assembled stack maintains optimal preload across the entire thermal operating range.
The 7212 base designation defines a 60x110x22 mm single-row angular contact ball bearing, but the suffixes dictate its survival in the field. The B suffix confirms the 40° contact angle, maximizing axial thrust capacity for vertical or heavily loaded shafts. The E designation indicates an optimized internal geometry with a larger ball complement, noticeably increasing the dynamic load rating without altering the outer envelope. The universal pairing capability (standardized as CB for heavy preload) allows these bearings to be mounted in any tandem, back-to-back, or face-to-face arrangement while maintaining a precise, pre-set internal clearance. Finally, the machined brass cage (standardized as M) provides superior durability and vibration damping compared to pressed steel alternatives, which is non-negotiable for precision spindle applications.
Substituting a standard clearance bearing for a universally paired, heavy preload variant might save money on the initial purchase order, but it guarantees unplanned downtime. When the spindle reaches operational speed, an improperly preloaded stack will experience axial play, leading to severe chatter marks on the machined parts and premature fatigue spalling on the raceways. The resulting equipment teardown, lost production hours, and replacement of damaged shafts and housings far exceed the cost of specifying the exact 7212 Becbm angular contact ball bearing from the start .
We do not simply pick boxes off a shelf; we actively audit the suffix alignment for every 7212 Becbm angular contact ball bearing order. Because lowercase suffix variations often cause cross-reference software to default to incorrect clearance classes, our engineers manually verify the universal pairing marks and preload specifications against your spindle requirements. We maintain authorized access to major international brands, meaning we can source the exact matched set you need without forcing compromises. Every shipment includes batch traceability, ensuring that the metallurgical integrity and dimensional accuracy meet the strict demands of high-speed precision equipment.
To ensure the 7212 Becbm angular contact ball bearing perfectly matches your application, please provide the specific spindle arrangement (DB, DF, or DT), the maximum operational RPM, and the expected axial thrust loads. If you are replacing an existing unit, sharing the OEM equipment number or the exact flushing marks on the current bearing outer rings allows our engineering team to verify the preload class and guarantee a seamless integration into your machine tool assembly.
Q: Why is the heavy preload class critical for the 7212 Becbm in spindle applications?
A: Heavy preload eliminates internal axial play, providing the extreme rigidity required for precision cutting and grinding. Without it, the spindle shaft will deflect under cutting forces, causing chatter, poor surface finishes, and accelerated fatigue failure on the bearing raceways due to uneven load distribution across the rolling elements.
Q: How do I verify the flush faces on a universal pairing bearing?
A: Universal pairing bearings feature specific V-marks or etched lines on the outer ring. When mounted back-to-back or face-to-face, these marks must align perfectly. This ensures the factory-ground flush faces mate correctly, establishing the precise internal clearance and preload designed into the 7212 Becbm configuration.
Q: Can I mix a 7212 Becbm with a different clearance class in the same spindle stack?
A: No. Mixing preload classes or internal clearances in a paired arrangement creates unequal load sharing. The bearing with the higher preload will carry the vast majority of the axial and radial forces, leading to rapid overheating, lubricant breakdown, and catastrophic seizure while the other bearing remains underutilized.
Q: What is the advantage of the machined brass cage over pressed steel in this designation?
A: The machined brass cage offers superior structural integrity, better heat dissipation, and enhanced vibration damping at high speeds. It maintains precise ball guidance under the heavy axial loads generated by the 40° contact angle, preventing cage deformation and ensuring reliable operation in demanding machine tool environments.
Q: How does your cross-reference process prevent suffix errors?
A: Automated catalogs often ignore critical pairing and cage suffixes, matching only the base 7212 dimension. Our engineers manually review the complete designation, verifying the contact angle, internal geometry optimization, preload class, and cage material to ensure the replacement bearing matches the exact mechanical and thermal requirements of your equipment.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.