01
Consultation
Technical needs assessment

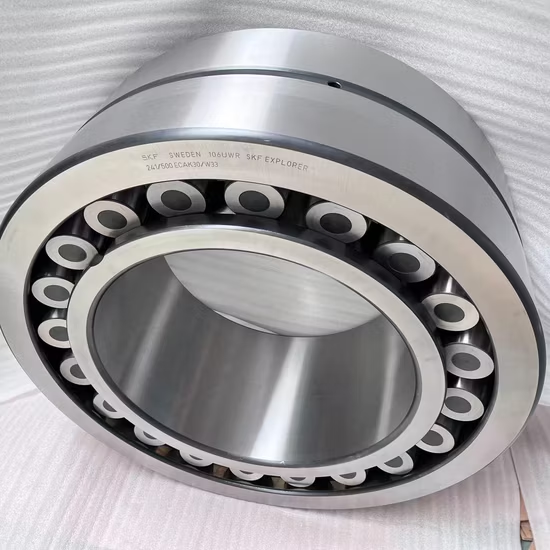
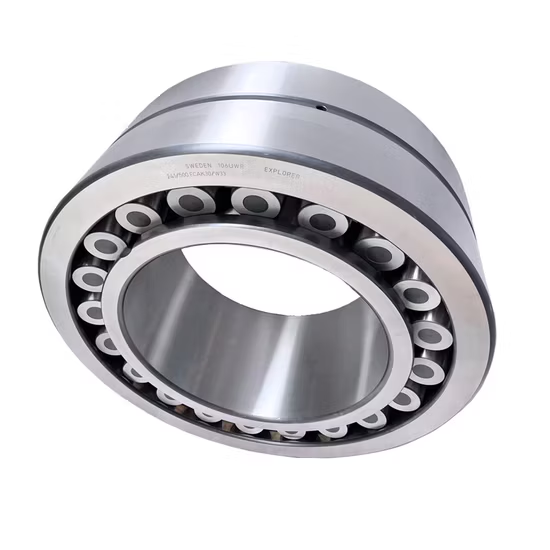

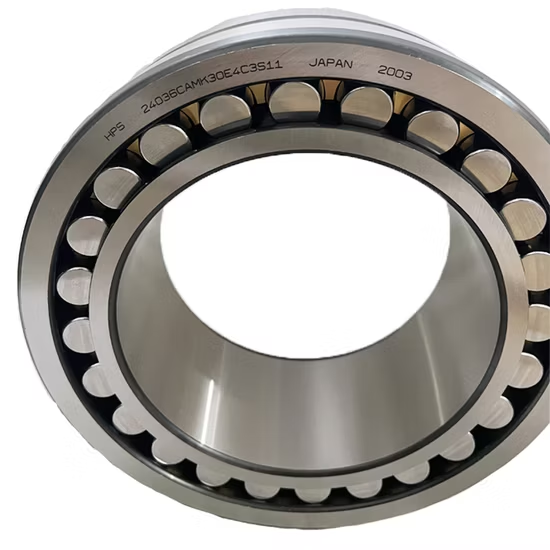
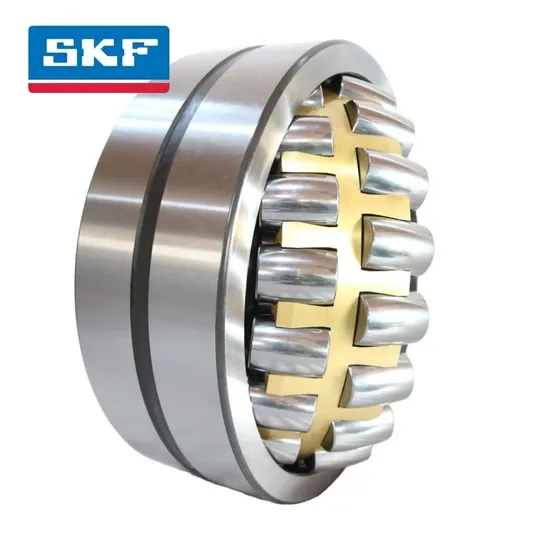
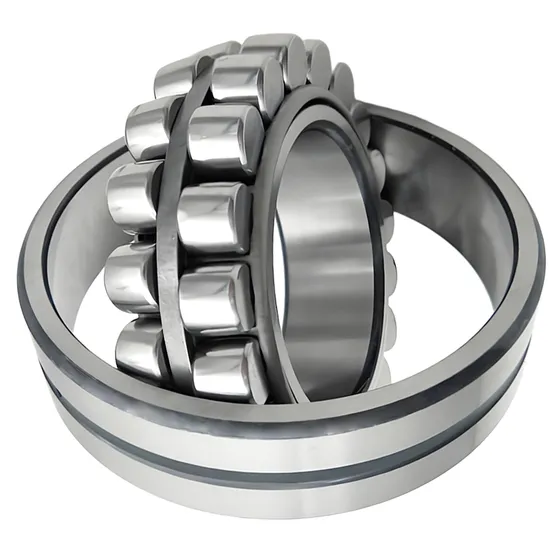
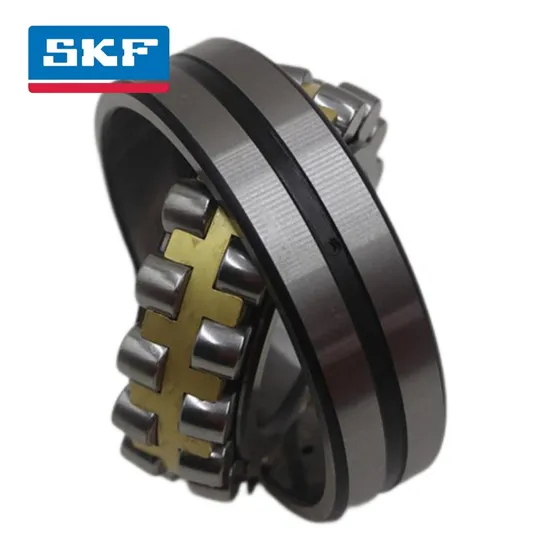
23060 Cak Cck W33/C3 Ma MB Spherical Roller Bearing featuring W33 outer ring lubrication grooves for optimal oil distribution in harsh environments.
Multi-Brand Authorized Coverage — Procure SKF, FAG, and NSK equivalents for the 23060 Cak Cck W33/C3 Ma MB in one consolidated shipment without juggling separate vendors.
| Parameter | Value |
|---|---|
| Designation | 23060 Cak Cck W33/C3 Ma MB |
| Bearing Type | Spherical Roller Bearing |
| Clearance Class | C3 (Greater than Normal) |
| Cage Material | Machined Brass (Inner Ring Guided) |
| Lubrication Feature | W33 (Outer Ring Groove and Holes) |
| Origin | Manufacturer dependent |
Note: Suffixes Cak, Cck, and Ma are unverified and require manufacturer catalog confirmation prior to final ordering.
| Industry | Typical Applications |
|---|---|
| Mining and Crushing | Jaw crusher eccentric shafts and vibrating screen mechanisms |
| Steel and Metallurgy | Continuous casting machine segments and rolling mill stands |
| Automotive and Heavy Vehicle | Heavy-duty suspension pivot points and articulation joints |
A missing clearance or lubrication suffix turns a heavy-duty component into a catastrophic failure point.
I once investigated a cement plant crusher in Dongguan that seized completely after just a few shifts. The previous supplier shipped a standard 23060 spherical roller bearing, ignoring the C3 clearance requirement. Under intense operational heat, the inner ring expanded, eliminating the internal gap and locking the shaft. In heavy industries, matching the base number is never enough; ignoring the W33 lubrication groove or the specific brass cage design leads to rapid thermal binding and cage disintegration .
When sourcing for mining or steel mill equipment, the 23060 spherical roller bearing must endure massive shock loads and heavy contamination. Our technical review process ensures that the selected variant aligns perfectly with your specific operational parameters. We verify that the internal geometry and cage construction can handle the severe radial forces typical in crushing and vibrating applications, preventing premature fatigue.
Crusher eccentric shafts and vibrating screens subject components to severe radial loads combined with intense structural vibrations. Operating temperatures frequently climb, demanding a C3 internal clearance to accommodate thermal expansion of the shaft and housing. Furthermore, heavy dust and slurry require consistent lubrication flow, making the W33 outer ring groove essential for distributing grease evenly. Without these specific design features, standard components quickly succumb to abrasive wear and thermal seizure .
The MB suffix indicates a machined brass cage guided by the inner ring, providing the structural integrity needed to survive heavy shock loads where stamped steel cages would deform. The W33 designation ensures an annular lubrication*sh grease to reach the rolling elements directly under load. Meanwhile, the C3 clearance class provides the necessary internal gap to prevent binding when the equipment reaches elevated operating temperatures.
Substituting a standard clearance bearing in a high-temperature application results in unplanned downtime and catastrophic damage to the surrounding housing. According to ISO 281 principles, ignoring the specific cage material or lubrication features drastically reduces the calculated fatigue life. A seized shaft in a continuous casting line or a primary crusher halts the entire production flow, leading to massive revenue losses far exceeding the initial component cost .
We supply authorized inventory across all major international brands, allowing you to fulfill mixed-brand requirements in a single order. Every 23060 Cak Cck W33/C3 Ma MB we dispatch includes full batch traceability to the original manufacturer. Our cross-brand interchange process strictly aligns the base designation, C3 clearance, and MB brass cage, rather than relying on superficial number matching. We also conduct an application-based selection review to confirm that the W33 lubrication design suits your specific maintenance intervals.
To ensure precise application matching, please share your operational parameters, including radial and axial loads, rotational speeds, and expected operating temperatures. This data allows our engineering team to validate the L10 fatigue life and confirm the suitability of the C3 clearance and MB cage design. If you are replacing an existing unit, providing the original OEM equipment number enables us to perform a comprehensive cross-reference check.
Q: Why does the base number match but the machine still fails?
A: Matching only the base number ignores critical internal design features. If a standard clearance bearing replaces a C3 variant in a high-temperature crusher, thermal expansion eliminates the internal gap, causing the shaft to seize. Similarly, missing the W33 lubrication groove starves the rolling elements of grease, leading to rapid cage failure under heavy loads.
Q: How do CN, C3, and C4 clearances differ in heavy machinery?
A: CN is standard clearance for normal temperatures and fits. C3 provides a larger internal gap, essential for applications with high operating temperatures or tight interference fits on the shaft to prevent thermal binding. C4 offers an even larger gap for extreme heat or specific vibrating screen applications where shaft expansion is highly significant.
Q: What is the difference between MB and MA brass cages?
A: The MB suffix designates a machined brass cage guided by the inner ring, which is highly effective in applications with heavy shock loads and moderate speeds. An MA cage is guided by the outer ring. The guidance method affects how the cage reacts to vibration and load zones, making the correct selection vital for maximizing fatigue life.
Q: Why choose a machined brass cage over stamped steel?
A: Machined brass cages offer substantially higher structural strength and wear resistance under heavy shock loads and severe vibrations. While stamped steel cages are lighter and suitable for standard applications, they can deform or fracture in demanding environments like mining crushers, making the robust brass design essential for reliability.
Q: What is the correct heating method for large spherical roller bearings?
A: Induction heaters are the preferred method for mounting large inner rings. The temperature must be carefully controlled and never exceed the thermal limit of the bearing steel to prevent annealing. Always measure the residual clearance after mounting to ensure the specified C3 gap remains intact and the bearing is not preloaded by the shaft fit.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.