01
Consultation
Technical needs assessment

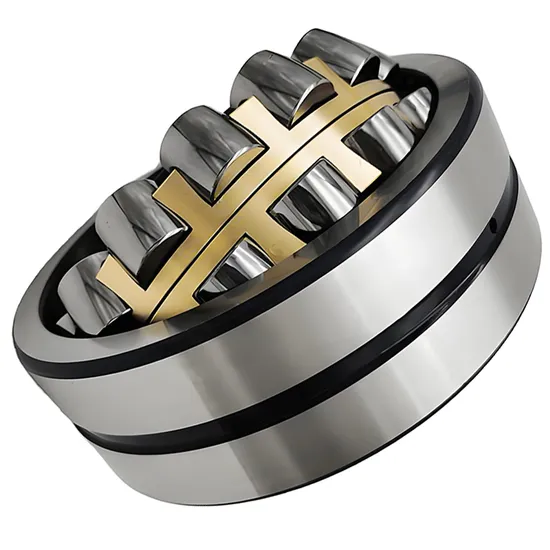
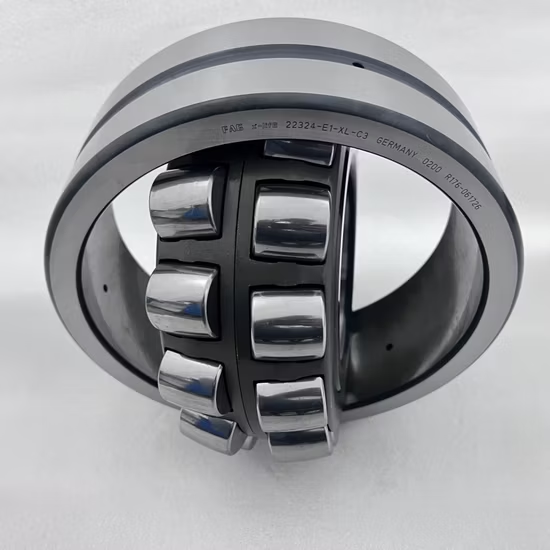
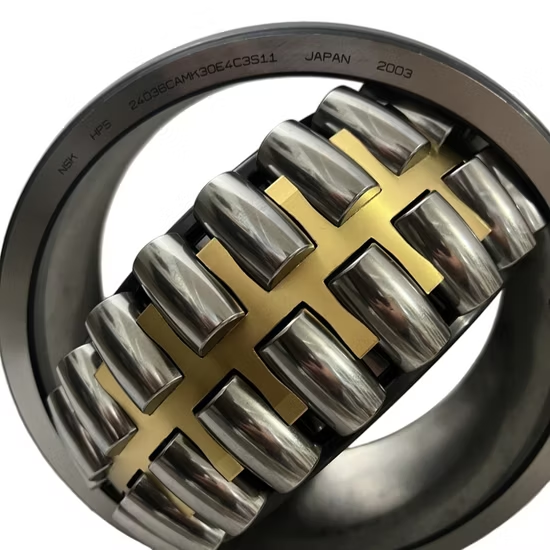
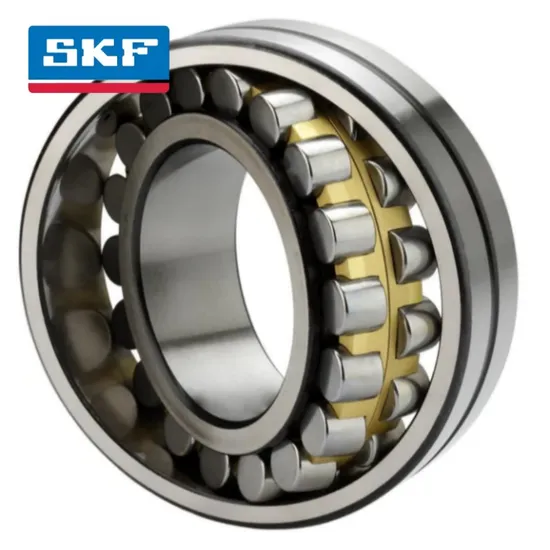
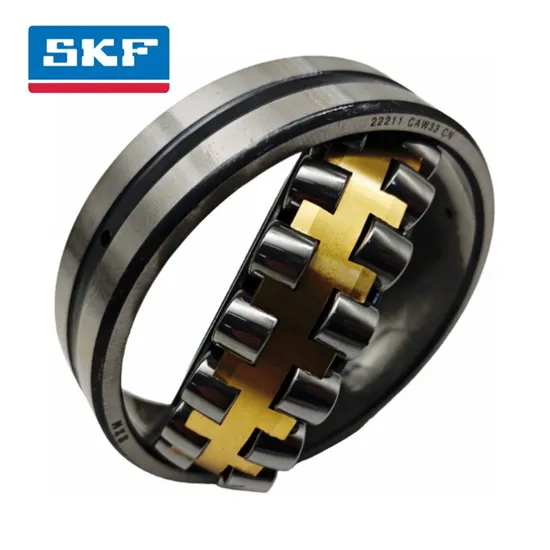
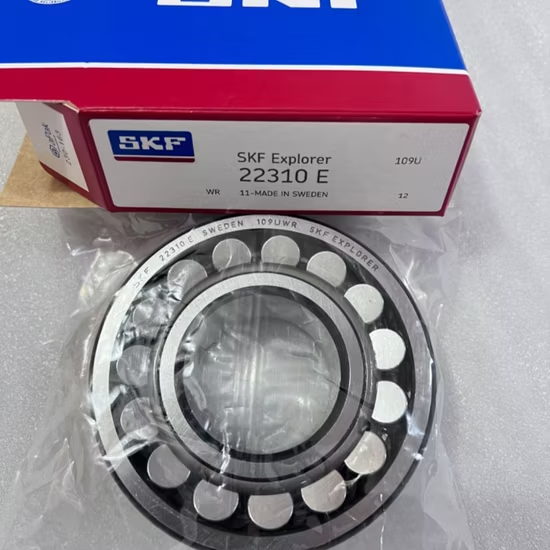
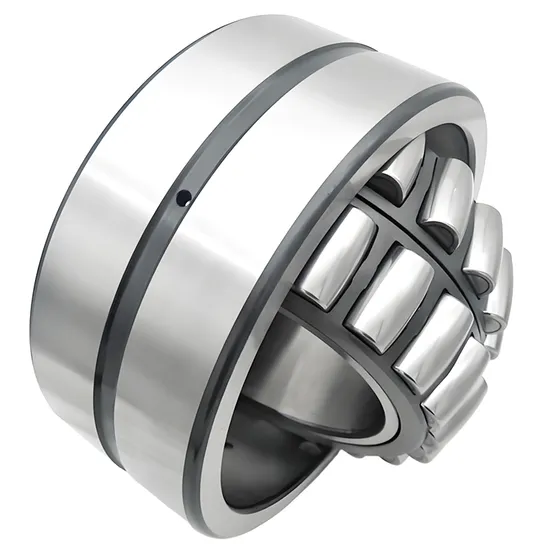
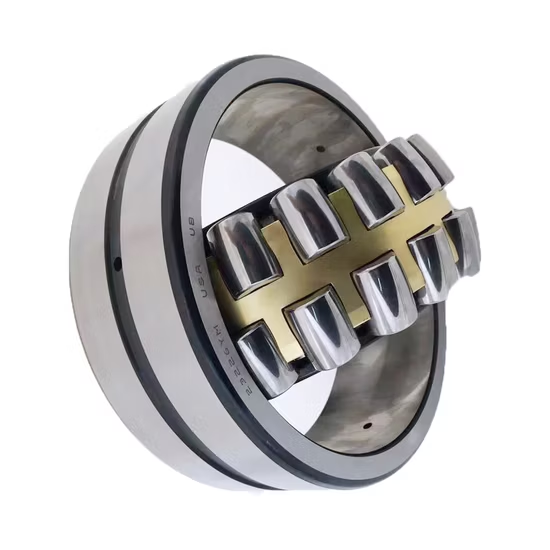
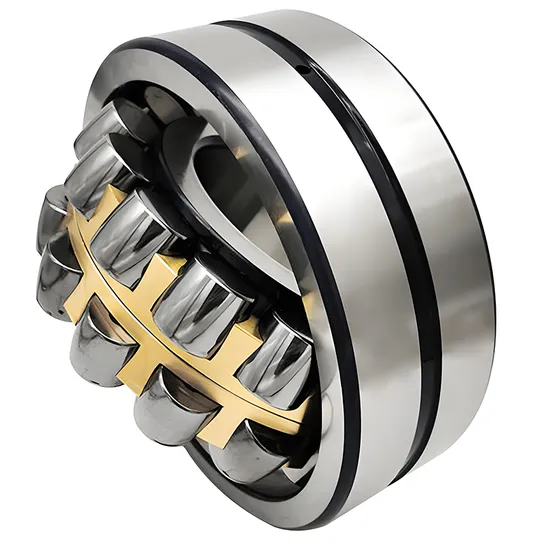
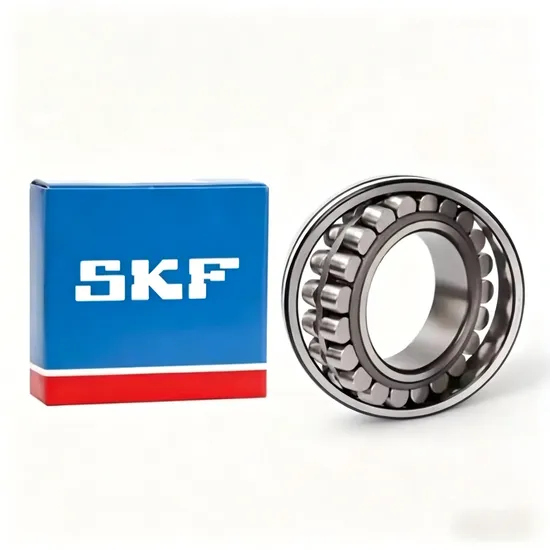
S K F 22314 Cc Ca Spherical Roller Bearing 70 mm bore
Cross-Reference Triad Alignment — We verify the base number, cage design, and clearance simultaneously to prevent catastrophic field failures in heavy-duty crushing equipment.
| Parameter | Value |
|---|---|
| Designation | S K F 22314 Cc Ca |
| Bearing Type | Spherical Roller Bearing |
| Bore Diameter (d) | 70 mm |
| Cage Material | Stamped steel, roller-guided (Cc) |
| Seal or Shield Type | Open |
| Clearance Class | Standard (CN) |
| Precision Class | P0 |
| Bore Type | Cylindrical |
| Industry | Typical Applications |
|---|---|
| Mining and crushing | Vibrating screen exciter mechanisms and primary jaw crusher toggle plates |
| Steel and metallurgy | Continuous casting machine roll guide units and cooling bed transfer gears |
| Industrial gearboxes | Heavy-duty extruder drive shafts and agitator support bearings |
Matching the internal design suffix is just as critical as getting the base dimensions right.
During a cement plant shutdown in Ethiopia, I traced a catastrophic gearbox seizure back to a simple cross-reference error. The maintenance team installed a spherical roller bearing with a machined brass cage where the OEM specifically required a stamped steel, roller-guided design. Under intense vibration, the incorrect cage material fatigued and fractured, locking the entire drive train. When sourcing a S K F 22314 Cc Ca spherical roller bearing, ignoring the cage suffix invites premature failure .
Heavy machinery demands internal components that withstand relentless shock loads. The stamped steel cage design in this S K F 22314 Cc Ca spherical roller bearing provides excellent structural stability and wear resistance in high-vibration environments like vibrating screens. Our engineering team reviews your specific load profiles to ensure the selected cage type and internal geometry align perfectly with the operational demands of your equipment.
Crushers and vibrating screens subject bearings to severe radial loads combined with intense, high-frequency shock impulses. These conditions generate significant internal friction heat, making the correct internal clearance vital to accommodate thermal expansion without causing roller binding. Furthermore, the open design requires a rigorous external lubrication schedule to flush out abrasive dust and prevent raceway scoring . Proper alignment during installation is equally crucial to prevent uneven load distribution across the roller profiles.
The 22314 base designation indicates a dimension series 23 bearing with a 70 mm bore, optimized for heavy radial and moderate axial loads. The Cc suffix specifies a stamped steel cage that is roller-guided, a configuration chosen for its ability to maintain precise roller alignment under severe vibration while minimizing internal friction. This cage type performs exceptionally well in applications where shock loads could otherwise deform weaker cage materials. The spherical outer ring raceway allows the inner ring and roller assembly to align slightly with the outer ring, compensating for shaft deflections or minor housing misalignments.
Installing a bearing with an unverified or mismatched internal design leads directly to unplanned downtime and catastrophic damage to surrounding shafts and housings. When a cage fails due to incorrect material selection for a high-vibration application, the rolling elements skew and jam, destroying the raceways instantly. Such failures void equipment warranties and force expensive emergency repairs. Adhering to ISO 281 life calculation standards requires exact specification matching, as even minor deviations in internal geometry drastically reduce the calculated fatigue life .
We do not just match base numbers; we verify the exact cage material and internal design to prevent the exact failures I have witnessed in the field. Every S K F 22314 Cc Ca spherical roller bearing we supply is cross-referenced against the OEM equipment manual to confirm the Cc stamped steel cage requirement. We provide full batch traceability directly from the manufacturer's production facilities, ensuring you receive genuine components. Our technical team reviews your application parameters to confirm that the standard clearance and precision class are appropriate for your specific operating temperatures and speeds.
To ensure optimal performance, please share your specific radial and axial load data, operating speeds, and ambient temperature ranges. This information allows our engineering team to verify the L10 fatigue life and confirm that the standard clearance is sufficient for your thermal expansion requirements. If you are replacing an existing component, providing the original equipment manufacturer part number enables us to perform a precise cross-reference check.
Q: Why must we verify the cage suffix during cross-referencing?
A: Base numbers only define external dimensions. The cage suffix dictates internal load distribution and vibration resistance. Installing a machined brass cage where a stamped steel Cc cage is required can alter internal clearances and cause catastrophic fatigue failure under high-frequency shock loads typical in crushing applications.
Q: How do we verify the authenticity of this specific bearing?
A: We supply original batch traceability documentation with every shipment. You can scan the QR code on the physical packaging using the manufacturer's official mobile application to instantly verify the production lot, origin, and genuine status of the component.
Q: What is the selection boundary between stamped steel and machined brass cages?
A: Stamped steel cages, like the Cc design, excel in high-vibration environments due to their lighter weight and structural resilience against shock loads. Machined brass cages are typically preferred for applications involving severe cage-guided friction, continuous high-speed rotation, or where chemical compatibility with specific synthetic lubricants is required.
Q: How should we handle the internal clearance during installation?
A: The standard clearance accommodates normal thermal expansion. During installation, avoid excessive cooling of the inner ring or overheating, as extreme temperature gradients can temporarily collapse the clearance, causing the rollers to bind against the Cc cage and damage the raceways before the equipment even starts.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.