01
Consultation
Technical needs assessment


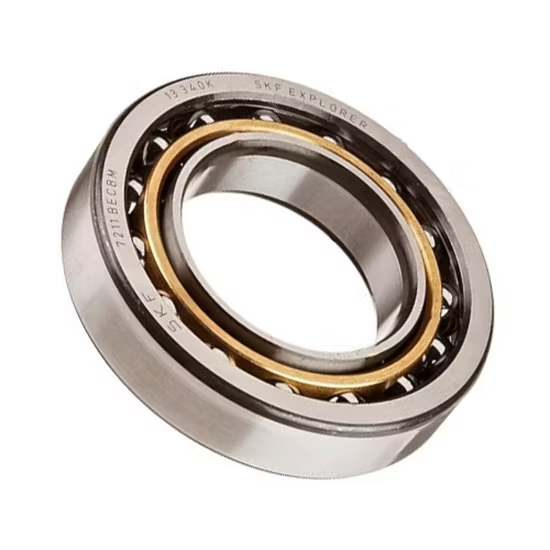
NSK 7014 CD/P4a Angular Contact Ball Bearing 70×110×20 mm — The 15° contact angle minimizes friction heat during high-speed operation, while P4a class guarantees strict running accuracy for machine tool spindles.
Multi-brand authorized coverage — Procure this precision spindle component alongside mixed-brand MRO requirements in a single traceable shipment without coordinating multiple suppliers.
| Parameter | Value |
|---|---|
| Designation | 7014 CD/P4a |
| Bearing Type | Angular Contact Ball Bearing |
| Bore Diameter (d) | 70 mm |
| Outside Diameter (D) | 110 mm |
| Width (B) | 20 mm |
| Contact Angle | 15° |
| Precision Class | P4a (ISO 492 Class 4 with enhanced running accuracy) |
| Material | Bearing Steel |
| Separated | Unseparated |
| Standards | ISO 492 |
| Industry | Typical Applications |
|---|---|
| Machine Tool Manufacturing | High-speed machining center spindles and precision grinding heads |
| Robotics & Automation | High-accuracy rotary joints and articulated arm pivot axes |
| Precision Equipment | Optical measuring instrument rotary tables and high-speed pump shafts |
A 15° optimized contact angle combined with P4a running accuracy prevents the thermal binding that destroys high-speed machining centers.
I have seen too many high-speed spindles scrapped because a standard precision bearing was swapped in during maintenance. When a machine tool spindle operates at high RPM, even microscopic deviations in running accuracy generate excessive friction heat. This heat causes the inner ring to expand, eliminating the carefully engineered internal clearance and leading to catastrophic thermal seizure. Sourcing an authentic NSK 7014 CD/P4a angular contact ball bearing ensures the dimensional tolerances strictly align with the spindle designer's thermal expansion calculations, preventing these costly unplanned downtime events .
The specific geometry of this NSK 7014 CD/P4a angular contact ball bearing makes it ideal for applications where high radial loads coincide with moderate axial thrust. The 15° contact angle provides a larger contact ellipse compared to steeper angles, distributing the load over a wider area of the raceway. This design minimizes localized stress and friction heat generation, which is exactly what high-speed precision equipment requires to maintain tight machining tolerances over long production runs.
At elevated rotational speeds, the friction heat generated inside the bearing envelope significantly alters the internal clearance. If the lubrication film breaks down or the grease degrades under thermal stress, the rolling elements will skid rather than roll. This skidding rapidly damages the raceway surfaces. Proper oil-air or oil-jet lubrication systems must be calibrated to manage this heat, ensuring the bearing steel components do not exceed their thermal limits while maintaining the hydrodynamic film required for P4a precision operation .
The "CD" suffix dictates the 15° contact angle, a critical parameter that balances axial load capacity with high-speed capability. The "P4a" designation goes beyond standard P4 dimensional tolerances; it guarantees enhanced running accuracy, meaning the radial and axial runout of the inner and outer rings are held to much tighter limits. This strict control over runout is what prevents the vibration harmonics that ruin surface finishes in precision grinding and milling operations.
Replacing a specified super precision component with a standard grade simply because the base numbers match is a recipe for disaster. The resulting vibration not only ruins the workpiece surface finish but also accelerates fatigue in the spindle housing and drive motors. According to failure analysis frameworks, these premature failures often trace back to incorrect internal geometry or poor running accuracy, leading to warranty voidance and massive production losses .
We focus on catching the exact cross-reference errors that cause field failures. A base number match is never enough; we verify that the 15° contact angle and P4a running accuracy suffixes perfectly align with your OEM specifications. Our inventory provides full batch traceability to the manufacturer, ensuring you receive genuine components. We also support cross-brand interchange reviews, confirming that any alternative part matches the exact clearance and precision requirements of your spindle design, eliminating the guesswork from critical MRO purchasing.
Share your specific spindle operating parameters, including maximum RPM, radial and axial cutting forces, and the chosen lubrication method. Our technical team will review these variables against the P4a precision limits to confirm this selection is optimal. If you are replacing an existing component, provide the exact OEM equipment number so we can perform a comprehensive cross-reference check, ensuring no critical suffix details are overlooked during the interchange process.
Q: How do I verify the authenticity of the P4a precision grade?
A: Every unit we supply features a unique QR code on the packaging. By scanning this code with the manufacturer's official mobile application, you can instantly verify the batch origin and confirm that the component meets the strict P4a running accuracy specifications. This digital traceability eliminates the risk of installing counterfeit parts that mimic standard visual markings but fail under high-speed thermal loads.
Q: What is the practical difference between P4 and P4a precision classes?
A: While both fall under the ISO 492 Class 4 dimensional umbrella, the P4a designation enforces significantly tighter controls on running accuracy. This means the radial and axial runout of the rings are minimized to a much greater degree. For high-speed machine tool spindles, this enhanced running accuracy is essential to prevent the microscopic vibrations that degrade machining surface finishes and accelerate fatigue.
Q: Why must the 15° contact angle match exactly during cross-referencing?
A: The contact angle determines how the bearing distributes loads between the radial and axial directions. Substituting a 25° or 40° angle variant alters the internal load distribution and stiffness characteristics of the spindle. This mismatch generates excessive friction heat at high speeds, leading to thermal expansion that destroys the internal clearance and causes premature seizure.
Q: Can I use this single bearing without a matched pair arrangement?
A: Yes, this specific designation is supplied as an unseparated, single-row component. However, in most high-speed spindle applications, single bearings are installed in sets with carefully calculated spacers to establish the required preload. Your spindle design documentation will dictate the exact mounting arrangement and preload forces needed to achieve the necessary system rigidity.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.