01
Consultation
Technical needs assessment




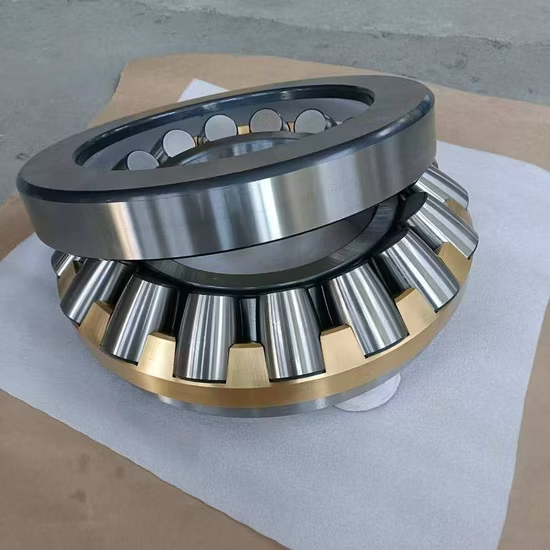
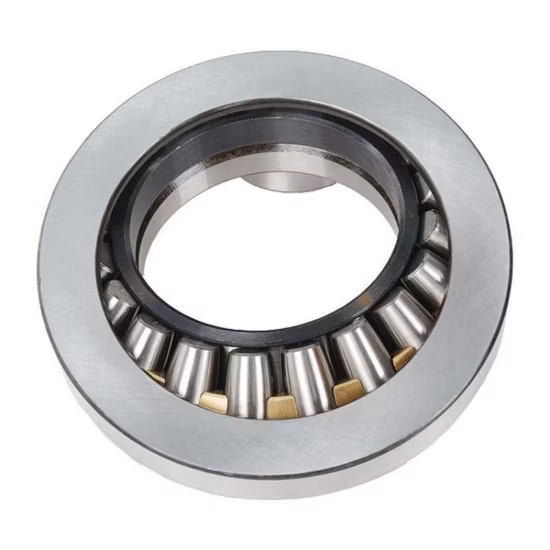
353166 C/Ha3 Single Direction Tapered Roller Thrust Bearing — designed to accommodate heavy axial loads in one direction while maintaining structural rigidity under extreme operational stress.
Verified Batch Traceability — Scan the manufacturer's official app QR code to confirm the exact metallurgical treatment of every 353166 C/Ha3 unit before it reaches your site.
| Parameter | Value |
|---|---|
| Designation | 353166 C/Ha3 |
| Bearing Type | Single Direction Tapered Roller Thrust Bearing |
| Origin | Germany / Japan / Sweden / Malaysia / China |
| HS Code | 8482500090 |
| Customization | Cross-reference support and exact suffix matching |
Note: Suffixes C and Ha3 require manufacturer catalog confirmation as specific design variants.
| Industry | Typical Applications |
|---|---|
| Mining and Crushing | Crusher main shaft thrust arrangements, gyratory crusher pivot points |
| Steel and Metallurgy | Continuous caster segment rolls, rolling mill screw-down mechanisms |
| Industrial Gearboxes | Heavy-duty extruder gearbox thrust support, mixer drive axial retention |
| Heavy-duty Material Handling | Crane hook block swivels, large capacity hoist drum thrust collars |
A minor deviation in internal design or heat treatment can trigger catastrophic cage failure under extreme axial loads, so how do you ensure the replacement part matches the OEM specification down to the last character?
Exact suffix alignment prevents thermal binding and premature structural collapse in heavy machinery.
I witnessed the aftermath of this exact oversight at a mining site in Latin America. A crusher main shaft seized completely due to overheating, and teardown revealed a shattered cage. The root cause was ignoring the specific heat treatment and clearance requirements tied to the 353166 C/Ha3 tapered roller thrust bearing suffixes. Procurement teams often match the base numbers but overlook the critical trailing characters, leading to severe operational disruptions .
Selecting the correct 353166 C/Ha3 tapered roller thrust bearing involves more than just verifying the bore and outside diameter. Our engineering review cross-checks the specific internal geometry and cage design against your equipment's actual axial load spectrum, ensuring the replacement component handles the dynamic forces without accelerated fatigue.
Crusher and mill environments subject thrust components to immense shock loading and heavy particulate contamination. The lubrication film must remain intact despite severe vibration, while the cage material must resist deformation during sudden load spikes. Proper heat treatment is essential to maintain dimensional stability when friction generates localized heat .
The Ha3 suffix typically designates a specialized heat treatment process applied to the rings or rolling elements, enhancing core toughness and surface hardness for shock absorption. The C suffix relates to internal clearance or specific contact geometry modifications. Installing a standard heat-treated part in an application demanding the Ha3 variant results in micro-cracking under impact, while ignoring the C suffix can cause thermal binding as the shaft expands during operation.
Substituting a standard thrust bearing where a specialized variant is required leads to unplanned downtime that far exceeds the component cost. The resulting cascade of damage often destroys adjacent seals, shafts, and housings, voiding equipment warranties and forcing emergency procurement at premium rates. Adhering to ISO 15243 failure analysis frameworks reveals that incorrect internal geometry is a primary driver of early fatigue spalling .
We prevent cross-reference errors by verifying not just the base designation, but the exact cage material and internal geometry required for your specific crusher or mill. Our multi-brand authorized network allows us to source the precise 353166 C/Ha3 tapered roller thrust bearing variant without forcing you to compromise on the suffix. Every shipment includes batch traceability to the manufacturer, eliminating the risk of counterfeit rings with soft inner cores that pass casual visual checks. We also review your application parameters to confirm the clearance class matches the thermal expansion characteristics of your housing.
To ensure accurate cross-referencing and selection, please provide the equipment OEM name, model number, and the exact operating parameters including axial load, rotational speed, and operating temperature. Sharing the original manufacturer's part number or a photo of the existing nameplate allows our engineering team to verify the suffix requirements and confirm the L10 life calculation for your specific application.
Q: How do I verify the authenticity and batch of the 353166 C/Ha3?
A: Every unit we supply features a unique QR code that links directly to the manufacturer's official verification app. Scanning this code confirms the batch number, production date, and specific heat treatment records, ensuring the component is genuine and fully traceable before installation.
Q: Why must I confirm the C/Ha3 suffix during cross-referencing?
A: Matching only the base number ignores critical internal design and heat treatment variations. The Ha3 suffix indicates specialized metallurgy for shock loads, while C defines internal geometry. Missing these details risks thermal binding or cage fracture under heavy axial stress.
Q: What causes premature failure in crusher thrust applications?
A: Failures typically stem from inadequate heat treatment, incorrect clearance selection, or lubrication breakdown under shock loads. Ensuring the replacement part matches the OEM's exact suffix requirements prevents micro-cracking and thermal seizure in high-vibration environments.
Q: What if the original OEM part with the Ha3 suffix is discontinued?
A: We utilize authorized cross-reference databases to identify equivalent variants from other major brands that meet the exact same metallurgical and dimensional specifications. Our team verifies the internal geometry and load ratings to ensure seamless interchangeability without compromising reliability.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.