01
Consultation
Technical needs assessment

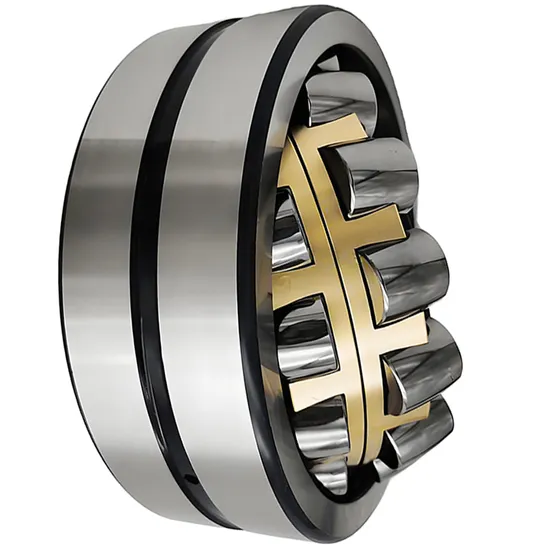
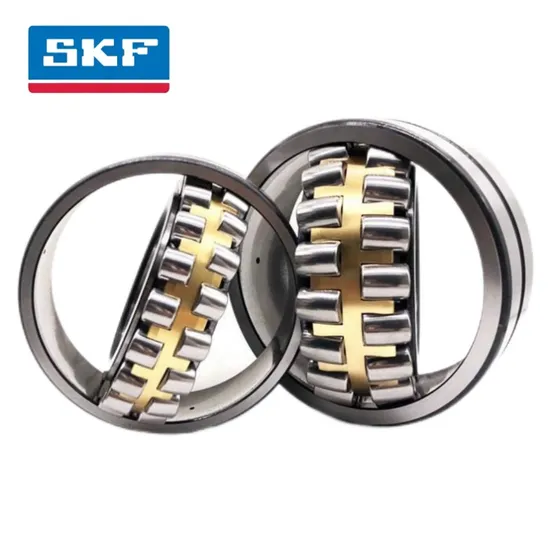
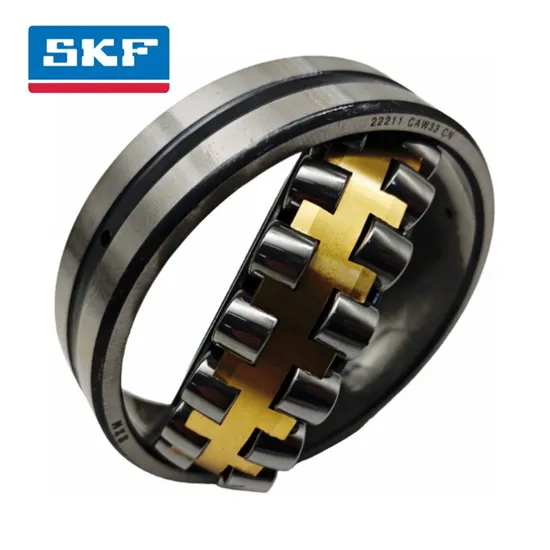
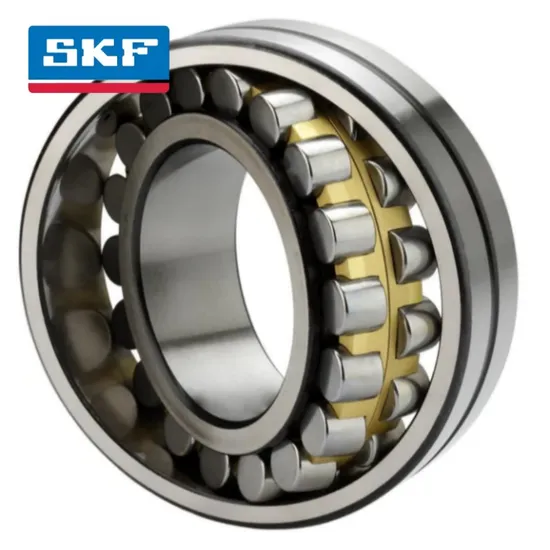
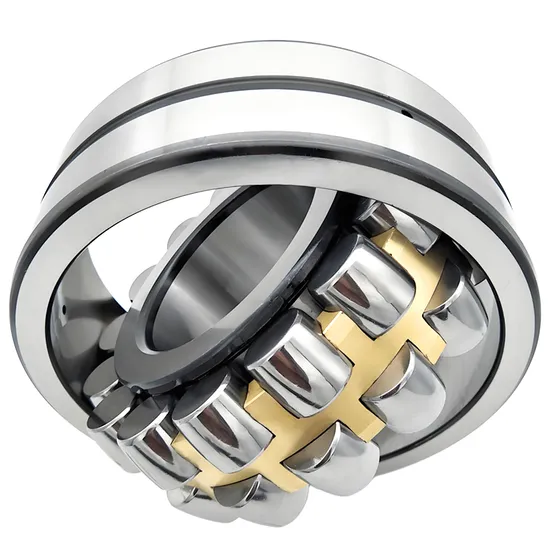
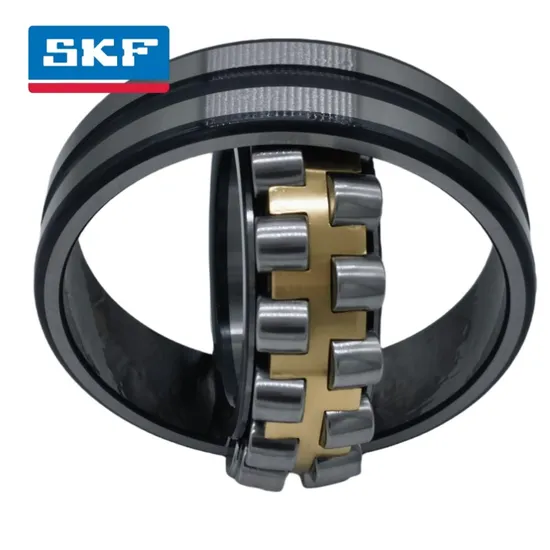
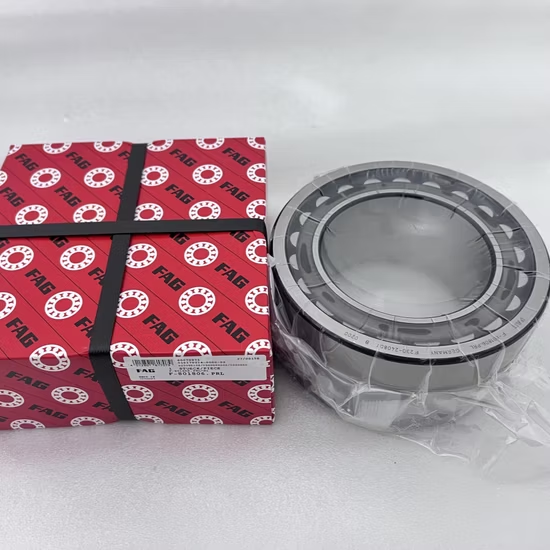
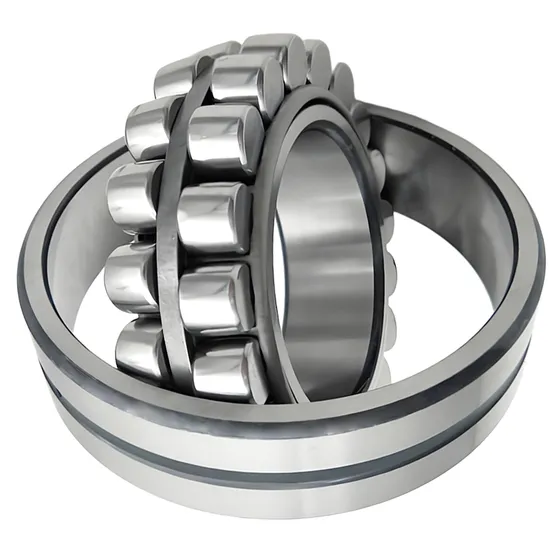
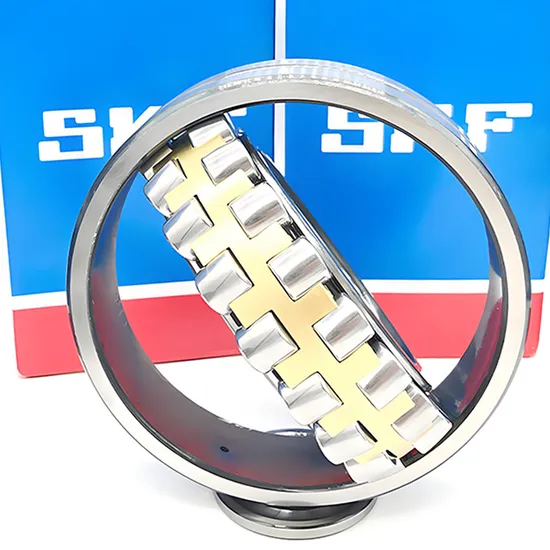
23996 MB/W33 Spherical Roller Bearing — equipped with a machined brass cage for heavy-load durability and outer ring lubrication grooves for consistent grease distribution in metallurgical applications.
Official App QR Verification — Scan the unique manufacturer code on every 23996 MB/W33 package to confirm authentic brass cage metallurgy before installation.
| Parameter | Value |
|---|---|
| Designation | 23996 MB/W33 |
| Bearing Type | Spherical Roller Bearing |
| Cage Material | Machined brass, inner ring guided (MB) |
| Lubrication Feature | Outer ring groove and holes (W33) |
| Origin | Germany / Japan / Sweden / Malaysia / China |
| Industry | Typical Applications |
|---|---|
| Metallurgical Equipment | Continuous casting machine rolls, cooling bed transfers |
| Steel Mill Equipment | Work roll necks, run-out table gearboxes |
| Heavy Machinery | Vibrating screens, primary crushers |
Suffix alignment dictates survival in extreme thermal and shock environments.
Sourcing a replacement based solely on the base dimension series often leads to catastrophic thermal binding on the shop floor. I have witnessed numerous 23996 MB/W33 spherical roller bearing installations fail prematurely because the procurement team overlooked the specific cage material and lubrication suffixes during cross-referencing. Substituting a standard stamped steel cage or omitting the outer ring lubrication groove in high-temperature rolling zones inevitably causes rapid cage fragmentation .
Securing the correct 23996 MB/W33 spherical roller bearing ensures the machinery can handle the punishing combination of heavy radial loads and severe misalignment typical in metal processing. Our technical review process verifies that the internal geometry and cage guidance system match the specific oscillating and shock loads of your equipment, preventing premature fatigue.
Continuous casting and hot rolling environments subject components to intense radiant heat, demanding adequate internal clearance to accommodate thermal shaft expansion. Without the W33 outer ring groove and holes, grease cannot reach the critical load zone, leading to localized overheating. Proper relubrication intervals and high-temperature grease selection are mandatory to prevent the rolling elements from skidding and smearing under these extreme thermal gradients .
The MB designation specifies a machined brass cage guided on the inner ring, providing superior structural integrity and resistance to shock loads compared to pressed steel alternatives. This rigid cage design maintains precise roller spacing even under severe vibration. Concurrently, the W33 feature integrates a circumferential groove and three lubrication holes in the outer ring, facilitating direct grease penetration into the roller paths. This combination is non-negotiable for heavy-duty applications where lubricant starvation triggers immediate operational failure.
Installing an alternative without the exact MB and W33 configuration voids warranty protections and guarantees unplanned downtime. A fragmented cage can jam the rolling elements, causing catastrophic damage to the shaft and housing. Addressing these secondary mechanical failures requires extensive line stoppages, far exceeding the initial component savings .
We maintain authorized distribution across all major international brands, allowing mixed-brand orders without compromising technical integrity. Our cross-reference protocol strictly aligns the MB cage material, W33 lubrication features, and internal clearance, rather than just matching the base bore and diameter. Every shipment includes batch traceability to the manufacturer, verified via official brand applications, effectively eliminating the risk of counterfeit rings with substandard metallurgy.
To ensure optimal performance, provide our engineering team with your specific radial and axial load profiles, operating temperatures, and rotational speeds. Supplying the original equipment manufacturer part numbers allows us to execute a precise cross-reference check, guaranteeing the replacement matches the exact internal geometry and suffix requirements of your metallurgical machinery.
Q: Why must the MB and W33 suffixes match exactly during cross-referencing?
A: Matching only the base dimensions ignores critical internal design features. The MB brass cage provides necessary shock resistance, while the W33 groove ensures adequate lubrication flow. Substituting these suffixes in heavy-duty metallurgical applications leads to rapid cage failure and thermal seizure.
Q: How does the MB machined brass cage outperform stamped steel in steel mills?
A: The machined brass cage offers significantly higher structural strength and wear resistance under heavy shock loads and vibration. Its inner-ring guided design maintains precise roller alignment, preventing the cage pockets from deforming and fragmenting under the extreme radial forces typical in rolling mills.
Q: What is the recommended relubrication strategy for the W33 outer ring design?
A: The W33 groove and holes allow grease to enter directly between the roller rows. In high-temperature continuous casting environments, operators should establish frequent, automated relubrication cycles using high-temperature synthetic greases to flush out contaminants and prevent lubricant starvation.
Q: How can I verify the authenticity of the bearing before installation?
A: Counterfeiters often clone packaging and QR codes. We provide complete batch traceability documentation, allowing you to scan the unique manufacturer code using the official brand application. This confirms the metallurgical authenticity of the rings and the precise machining of the brass cage.
Q: What are the correct heating parameters for mounting this large spherical roller bearing?
A: Large bore bearings require uniform induction heating to expand the inner ring for a slip fit. The temperature must be carefully monitored to avoid exceeding the thermal limits of the bearing steel or damaging the MB brass cage, ensuring the correct residual clearance is maintained after cooling.
Our 5-step process ensures every order is engineered, validated, and supported for optimal performance.
Technical needs assessment
Custom specifications
Free samples for $50k+
Pre-shipment inspection
On-site & predictive
Our certified engineers respond within 24 hours with detailed technical specifications, pricing, and lead time information.